
>99.5% purity
Typical purified bromine product for process reuse.
Recovery and purification plants producing reusable bromine from industrial HBr, sodium-bromide, potassium-bromide and aqueous waste streams.
UD Technologies · Vadodara, India
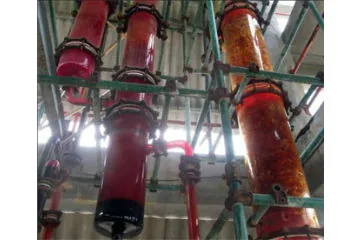
Industrial bromide recovery
Typical purified bromine product for process reuse.
Recover from HBr, NaBr, KBr and aqueous waste.
Reduce bromine purchase and waste-treatment demand.
Condition feeds containing process organics.
Salient features
The final equipment arrangement, materials and controls are selected around the process duty and site conditions.
Chlorine oxidation and live steam release bromine from aqueous bromides.
Cooling and chilling exchangers condense bromine-rich overhead vapour.
A glass separator divides condensed bromine from the aqueous phase.
Reboiling and fractional distillation raise crude bromine to reuse quality.
Glass and compatible materials are applied throughout the aggressive service.
PLC control and application-specific instrumentation can be integrated.
System configuration
The plant is engineered as one coordinated system, with pretreatment and final drying added where the feed and product specification require them.
Related system
For salt-field brines, the sea-bittern production plant is engineered around variable natural feed concentration and hot reactive stripping.
Discuss your requirements